Next-Generation Ceramics: Unlocking Superior Properties for Industry

PRODUCT PARAMETERS
Description
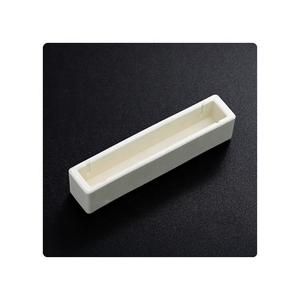
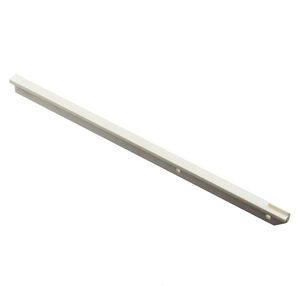
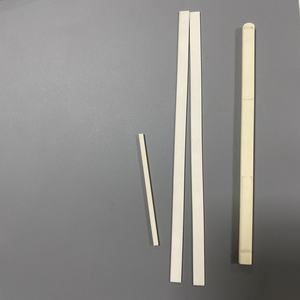
Overview of Alumina Ceramic Refractory Shaft for Pumps
Alumina Ceramic, or Aluminum Oxide (Al₂O₃), is the most widely used and versatile advanced ceramic material. Known for its excellent balance of mechanical, thermal, and electrical properties, it is a cost-effective solution for a vast array of demanding industrial applications. Alumina components are produced in purity levels ranging from 85% to 99.9%, with properties enhancing as purity increases.
Features of Alumina Ceramic Refractory Shaft for Pumps
- High Hardness & Wear Resistance: Offers exceptional resistance to abrasion and mechanical wear.
- Excellent Electrical Insulation: Maintains high electrical resistivity even at elevated temperatures.
- Good Thermal Conductivity: (For a ceramic) effectively dissipates heat, especially in higher purity grades.
- High Compressive Strength: Capable of withstanding significant mechanical loads.
- Chemical Inertness: Highly resistant to corrosion from acids, alkalis, and molten metals.
- Cost-Effectiveness: Provides superior performance at a lower cost compared to many other technical ceramics.
Specifications of Alumina Ceramic Refractory Shaft for Pumps
This alumina ceramic refractory shaft is developed for challenging pump jobs. It deals with high warm and severe chemicals well. The main material is high-purity alumina ceramic. This things is extremely tough and stands up to obtaining worn down. Its thickness is high. This makes it strong versus influences and squashing forces. Warmth resistance is a big deal. This shaft functions penalty in really warm places. It will not split or break down quickly under heats. The ceramic does not respond with many chemicals. Acids and alkalis generally do not hurt it. This means the shaft lasts much longer in rough problems. Mechanical strength is superb. It bears heavy lots without bending or breaking. The shaft maintains its shape under stress. Dimensional accuracy is essential for pumps. We make these shafts to very close dimension restrictions. This makes sure an ideal fit with pump components. Surface finish is smooth. A smooth surface area aids the shaft spin quickly. It additionally reduces wear on seals and bearings. Use resistance is superior. The alumina ceramic fights off abrasion far better than metal. This is crucial for pumps relocating abrasive fluids. Deterioration resistance is top-notch. The ceramic does not corrosion or corrode. This is necessary for pumps handling salt water or chemicals. Electrical insulation buildings are excellent. The shaft does not conduct power. This is useful in unique electric atmospheres. The alumina ceramic keeps stable. Its size does not alter much with temperature level changes. This maintains the pump running precisely. We evaluate every shaft very carefully. We examine the hardness, stamina, and dimension. This assures top quality and integrity. These shafts fit many challenging pump applications. They function well in chemical transfer pumps. They are good for abrasive slurry pumps. They carry out in high-temperature oil pumps. They serve sought after commercial tasks. This shaft provides a long lasting option. It decreases downtime and upkeep expenses. It boosts pump efficiency and life-span.
Applications of Alumina Ceramic Refractory Shaft for Pumps
Alumina ceramic refractory shafts are excellent for hard pump jobs. They deal with rough chemicals well. Acids and antacid reason problems for metal shafts. These ceramic shafts resist rust much better. This means longer life and less downtime.
Warmth is another large issue in several sectors. Alumina ceramic handles heats easily. It won’t warp or thaw like metal can. Pumps remain reliable even in hot problems.
Use is a continuous challenge. Slurries and abrasive fluids wear down steel parts fast. Alumina ceramic is really difficult. It takes on abrasion a lot longer. You won’t require to replace these shafts as often.
Electrical insulation is an additional benefit. Steel shafts can conduct electricity. This is dangerous in some settings. Alumina ceramic is non-conductive. It adds safety and security to the pump operation.
These shafts also keep things tidy. They withstand chemical attack. This avoids contamination. Products remain pure. This is crucial for food or pharmaceutical usages.
The product stays secure. It does not change dimension much with warmth. This keeps pump seals tight. Leaks are less most likely. Performance remains constant.
Installation is straightforward. They fit standard pump styles. Upkeep is simpler as well. Less corrosion ways less frequent checks. Operators save money and time.
Overall, alumina ceramic refractory shafts are a smart option. They deal with rust, heat, and put on effectively. Pumps run longer and much better. Industries obtain more reputable efficiency.

Company Profile
Synthetic-chemical focus on the research and development, production and sales of ceramic products, serving the electronics, ceramics, chemical and other industries. Since its establishment in 2015, the company has been committed to providing customers with the best products and services, and has become a leader in the industry through continuous technological innovation and strict quality management.
Our products includes but not limited to Aluminum Nitride, Aluminum Oxide, Boron Carbide, Boron Nitride, Ceramic Crucible, ect. If you are interested in any type of these, please feel free to contact us.

Payment Methods
T/T, Western Union, Paypal, Credit Card etc.
Shipment Methods
By air, by sea, by express, as customers request.
5 FAQs of Alumina Ceramic Refractory Shaft for Pumps
What is an alumina ceramic refractory shaft made of?
It’s primarily made from alumina, a very hard ceramic material. Alumina offers excellent resistance to wear and chemicals. This makes the shaft tough and durable.
Why use ceramic instead of metal for pump shafts?
Ceramic handles tough conditions better than metal. It doesn’t rust or corrode easily. It also stands up to abrasive liquids much longer. Metal wears out faster in these situations.
Where are these ceramic shafts typically used?
They are used in pumps moving harsh liquids. Examples include chemical processing, mining slurries, and wastewater treatment. These environments need materials that last under stress.
What are the main benefits?
The biggest benefit is much longer service life. Less downtime for replacements saves money. Better resistance to corrosion and wear improves pump reliability. Performance stays high.
Do these shafts need special care?
They require careful handling during installation. Avoid impacts or shock loads. Proper alignment in the pump is crucial. Once installed, they need little extra maintenance.
REQUEST A QUOTE
RELATED PRODUCTS
Medium Sodium Calcined Alumina Powder (99.3%-99.85%) for Ceramics & Coatings
High Bulk Density White Fused Alumina Aggregates for Refractory Industry
High-Temperature Stable (Withstands 1800°C) Alumina Microspheres for Refractories
95% Alumina Ceramic Mining Square Mosaic Tile with Dimples
Factory Alumina Grinding Media Balls / Tumbling Media