Next-Generation Ceramics: Unlocking Superior Properties for Industry

PRODUCT PARAMETERS
Description
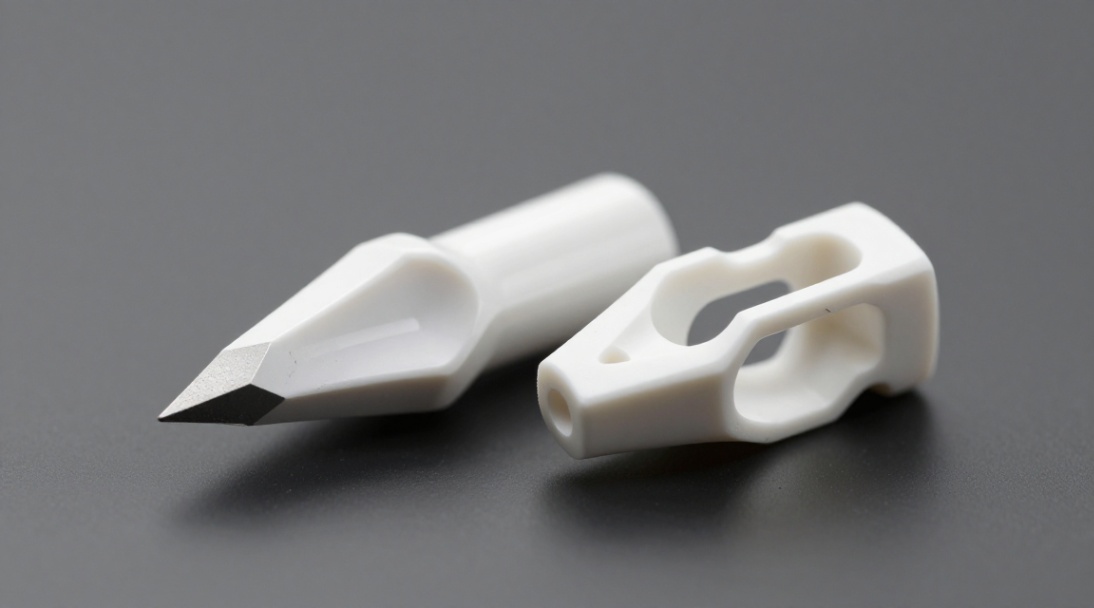
Overview of Alumina Ceramic Shaft & Bushing for Oxygen Sensors
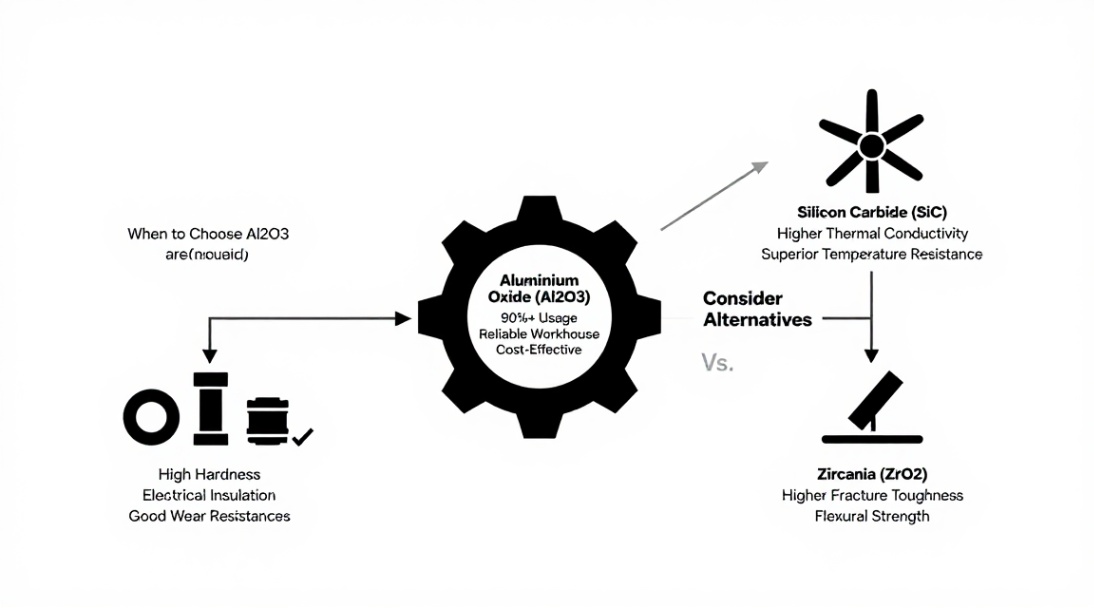
Alumina Ceramic, or Aluminum Oxide (Al₂O₃), is the most widely used and versatile advanced ceramic material. Known for its excellent balance of mechanical, thermal, and electrical properties, it is a cost-effective solution for a vast array of demanding industrial applications. Alumina components are produced in purity levels ranging from 85% to 99.9%, with properties enhancing as purity increases.
Features of Alumina Ceramic Shaft & Bushing for Oxygen Sensors
- High Hardness & Wear Resistance: Offers exceptional resistance to abrasion and mechanical wear.
- Excellent Electrical Insulation: Maintains high electrical resistivity even at elevated temperatures.
- Good Thermal Conductivity: (For a ceramic) effectively dissipates heat, especially in higher purity grades.
- High Compressive Strength: Capable of withstanding significant mechanical loads.
- Chemical Inertness: Highly resistant to corrosion from acids, alkalis, and molten metals.
- Cost-Effectiveness: Provides superior performance at a lower cost compared to many other technical ceramics.
Specifications of Alumina Ceramic Shaft & Bushing for Oxygen Sensors
Alumina Porcelain Shaft & Bushing for Oxygen Sensors
Product and Structure
These components are made from high-purity alumina ceramic (Al two O ₃), with a pureness degree of 96% or greater. The material uses excellent electrical insulation, strong resistance to deterioration, and secure efficiency at heats. It does not respond with oxygen or exhaust gases, that makes it ideal for usage in severe sensor settings.
Secret Specifications
The shaft and bushing are precision-engineered to limited resistances. Criterion external diameters vary from 2 mm to 10 mm, while internal sizes can be tailored based upon sensing unit style requirements. Sizes commonly drop between 5 mm and 50 mm. Surface finish is smooth, with a roughness standard (Ra) of ≤ 0.8 µm, making certain marginal friction and wear throughout procedure.
Running temperature capability expands as much as 1600 ° C in air. Thermal growth is low and consistent, assisting preserve dimensional stability under duplicated home heating and cooling cycles. The components also reveal high mechanical stamina, with a flexural strength of 300– 350 MPa and firmness above 1500 HV.
Efficiency Includes
Chemical inertness: Stands up to assault from acids, alkalis, and combustion by-products.
Electric insulation: Maintains dielectric strength also at raised temperatures.
Thermal shock resistance: Takes care of quick temperature adjustments without cracking.
Long life span: Resilient framework lowers maintenance and replacement regularity.
Applications
These ceramic shafts and bushings are utilized mostly in automobile and industrial oxygen sensors. They sustain exact oxygen dimension in exhaust systems, combustion control systems, and emission tracking tools. Their integrity makes sure constant sensor outcome over time, also in hostile operating problems.
Applications of Alumina Ceramic Shaft & Bushing for Oxygen Sensors
Applications of Alumina Porcelain Shaft & Bushing for Oxygen Sensors
Why Alumina Ceramic Functions Best
Oxygen sensors need parts that can deal with hard conditions. High heat, harsh gases, and consistent stress and anxiety prevail in engine exhaust systems. Alumina ceramic takes on all of this. It keeps its form and stamina even at really heats. It also stands up to chemical wear from exhaust fumes.
Shaft and Bushing Functions
The ceramic shaft holds the sensor component in place. It needs to remain secure while the engine vibrates. Alumina ceramic does not increase a lot when hot. This indicates the sensing unit stays straightened and works properly in time.
The ceramic bushing serves as a seal and assistance. It shields electrical connections inside the sensing unit. At the exact same time, it allows exhaust gas reach the noticing surface area. Alumina’s tight framework obstructs leaks but enables appropriate gas circulation through developed paths.
Real-World Use Instances
Auto manufacturers make use of these components in automotive oxygen sensing units . They assist engines run cleaner and extra effectively. The ceramic elements last much longer than steel or plastic alternatives. This decreases the requirement for repair work and replacements.
In industrial burning systems , such as central heating boilers or furnaces, oxygen sensors keep an eye on air-fuel mixtures. Alumina ceramic shafts and bushings ensure dependable readings under continuous high heat. Manufacturing facilities depend on this security to fulfill safety and security and exhausts regulations.
Also in marine and power generation engines , these ceramic components play a crucial role. Salt, moisture, and warm challenge most products. Alumina ceramic manages them without deteriorating.
Trick Benefits at a Glimpse
– High thermal security : Works well above 1000 ° C.
– Chemical inertness : Resists corrosion from acidic or basic gases.
– Electric insulation : Keeps sensing unit signals tidy and accurate.
– Mechanical strength : Holds tight resistances despite resonance.
These traits make alumina ceramic the leading choice for oxygen sensing unit shafts and bushings throughout numerous requiring fields.

Company Profile
Synthetic-chemical focus on the research and development, production and sales of ceramic products, serving the electronics, ceramics, chemical and other industries. Since its establishment in 2015, the company has been committed to providing customers with the best products and services, and has become a leader in the industry through continuous technological innovation and strict quality management.
Our products includes but not limited to Aluminum Nitride, Aluminum Oxide, Boron Carbide, Boron Nitride, Ceramic Crucible, ect. If you are interested in any type of these, please feel free to contact us.

Payment Methods
T/T, Western Union, Paypal, Credit Card etc.
Shipment Methods
By air, by sea, by express, as customers request.
5 FAQs of Alumina Ceramic Shaft & Bushing for Oxygen Sensors
Why choose alumina ceramic for oxygen sensor shafts and bushings?
Alumina ceramic offers excellent heat resistance and electrical insulation. It stays stable at high temperatures found in exhaust systems. This material also resists corrosion from harsh gases, which helps the oxygen sensor work reliably over time.
How does alumina ceramic improve sensor performance?
The ceramic’s thermal stability keeps the sensor’s internal parts protected. It prevents unwanted electrical signals by blocking current leakage. This means the sensor sends accurate readings to the engine control unit, supporting better fuel efficiency and lower emissions.
Can these components handle extreme temperature changes?
Yes. Alumina ceramic handles rapid heating and cooling without cracking. Its low thermal expansion reduces stress during temperature swings. This durability is key in automotive exhaust environments where conditions change quickly.
Are alumina ceramic shafts and bushings easy to install?
They fit standard oxygen sensor designs without extra steps. Their precise dimensions match OEM specs, so no special tools or adjustments are needed. Just replace like any other sensor part.
What makes alumina better than metal or other ceramics?
Metal parts can corrode or conduct electricity, which harms sensor accuracy. Other ceramics may lack strength or thermal resistance. Alumina ceramic combines hardness, insulation, and chemical stability in one reliable package. That’s why it’s widely used in demanding automotive applications.
REQUEST A QUOTE
RELATED PRODUCTS
Calcined Alumina / Polishing Aluminum Oxide Powder (CAS 1344-28-1)
Custom High Purity Pink Alumina (Al2O3) Ceramic Wafer / Substrate
0.1mm/0.2mm Lapped 99.6% Alumina (Al2O3) Ceramic Substrate
95% Alumina Ceramic Wafer / Insulating Al2O3 Substrate
Low Sodium Microcrystalline Alumina Powder for Ceramic Components