Next-Generation Ceramics: Unlocking Superior Properties for Industry

PRODUCT PARAMETERS
Description
Overview of 99% High Alumina Ceramic Ball for Catalyst Support
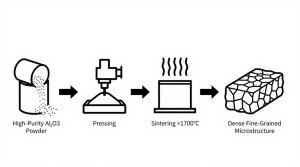
Alumina Ceramic, or Aluminum Oxide (Al₂O₃), is the most widely used and versatile advanced ceramic material. Known for its excellent balance of mechanical, thermal, and electrical properties, it is a cost-effective solution for a vast array of demanding industrial applications. Alumina components are produced in purity levels ranging from 85% to 99.9%, with properties enhancing as purity increases.
Features of 99% High Alumina Ceramic Ball for Catalyst Support
- High Hardness & Wear Resistance: Offers exceptional resistance to abrasion and mechanical wear.
- Excellent Electrical Insulation: Maintains high electrical resistivity even at elevated temperatures.
- Good Thermal Conductivity: (For a ceramic) effectively dissipates heat, especially in higher purity grades.
- High Compressive Strength: Capable of withstanding significant mechanical loads.
- Chemical Inertness: Highly resistant to corrosion from acids, alkalis, and molten metals.
- Cost-Effectiveness: Provides superior performance at a lower cost compared to many other technical ceramics.
Specifications of 99% High Alumina Ceramic Ball for Catalyst Support
99% High Alumina Ceramic Sphere for Catalyst Support
Product and Composition
These ceramic balls are made from 99% pure light weight aluminum oxide (Al ₂ O FOUR). The high alumina web content gives them strong mechanical residential properties and excellent resistance to warm and chemicals. They consist of extremely few impurities, which assists keep stable performance sought after industrial environments.
Physical Properties
Density: Around 3.6 g/cm THREE.
Hardness: Mohs solidity of 9, making them extremely resistant to put on.
Compressive toughness: Over 2,000 MPa, so they can handle hefty tons without damaging.
Thermal expansion coefficient: Low, at around 7.5 × 10 ⁻⁶/ ° C, which suggests they stay secure under temperature modifications.
Thermal and Chemical Resistance
The spheres work well in temperatures approximately 1,750 ° C. They do not react with most acids, alkalis, or solvents. This makes them secure to make use of in chemical processing, petrochemical refining, and other harsh setups. Their inert nature protects against undesirable side responses with stimulants or process materials.
Size and Resistance
Standard diameters vary from 3 mm to 25 mm. Customized sizes are additionally readily available. Each ball is formed with tight dimensional control. Size tolerance stays within ± 0.1 mm to guarantee uniform packing and constant circulation in activators.
Surface area and Structure
The surface is smooth and free of splits or pits. The inner structure is dense and non-porous. This design stops liquids or gases from obtaining caught inside, which assists maintain the stimulant support clean and reliable.
Applications
These balls are widely used as assistance media underneath stimulant beds in fixed-bed activators. They help spread gas or fluid equally across the driver layer. Industries like oil refining, plant food manufacturing, and ecological design rely upon them for trustworthy, lasting operation.
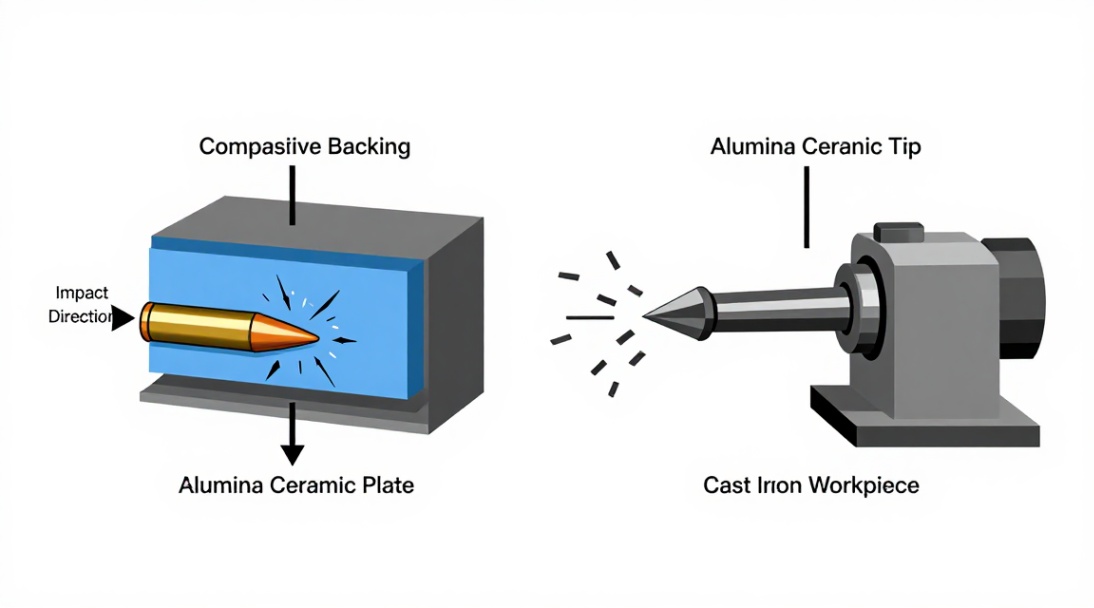
Applications of 99% High Alumina Ceramic Ball for Catalyst Support
Applications of 99% High Alumina Porcelain Balls for Stimulant Assistance
Why These Ceramic Balls Work Well
99% high alumina ceramic balls are made mostly from aluminum oxide. This gives them strong heat resistance and chemical stability. They do not break down conveniently when subjected to extreme chemicals or high temperatures. That makes them perfect for use in commercial reactors where stimulants must remain energetic over extended periods.
Where They Are Utilized
These ceramic spheres are typically made use of as driver assistance media in petrochemical plants, refineries, and chemical processing systems. They hold the real driver product in place while allowing gases or liquids flow through evenly. This aids reactions take place much faster and more completely. In ammonia synthesis, hydrogen manufacturing, and sulfur recovery devices, these balls keep the system running smoothly.
Secret Conveniences in Real Workflow
One big advantage is their high mechanical toughness. They can manage heavy loads without breaking or using down. This minimizes the need for regular substitutes and decreases maintenance costs. Their smooth surface additionally protects against unwanted accumulation of carbon or other down payments.
Because they are chemically inert, they do not respond with the catalyst or process fluids. This keeps the response tidy and prevents side products. Their uniform shapes and size make sure consistent circulation distribution, which improves total performance.
Efficiency Under Tough Problems
In atmospheres over 1,000 ° C or under solid acidic or alkaline problems, numerous products fall short. 99% alumina ceramic spheres maintain functioning without losing shape or function. Plants that run nonstop rely on this reliability. Operators trust them to keep pressure decrease stability and stop channeling in fixed-bed activators.

Company Profile
Synthetic-chemical focus on the research and development, production and sales of ceramic products, serving the electronics, ceramics, chemical and other industries. Since its establishment in 2015, the company has been committed to providing customers with the best products and services, and has become a leader in the industry through continuous technological innovation and strict quality management.
Our products includes but not limited to Aluminum Nitride, Aluminum Oxide, Boron Carbide, Boron Nitride, Ceramic Crucible, ect. If you are interested in any type of these, please feel free to contact us.

Payment Methods
T/T, Western Union, Paypal, Credit Card etc.
Shipment Methods
By air, by sea, by express, as customers request.
5 FAQs of 99% High Alumina Ceramic Ball for Catalyst Support
Frequently Asked Questions About 99% High Alumina Ceramic Balls for Catalyst Support
What is a 99% high alumina ceramic ball?
This ball is made from aluminum oxide with a purity of 99%. It is very hard, strong, and stable at high temperatures. People use it mainly to support catalysts in chemical reactors.
Why choose 99% alumina over lower grades?
Higher alumina content means better performance. These balls resist heat, wear, and chemicals much better than balls with less alumina. They last longer and keep their shape under tough conditions.
Where are these ceramic balls used?
They work inside reactors, towers, and vessels in industries like petrochemicals, fertilizers, and refining. Their main job is to hold catalyst materials evenly so reactions happen smoothly and safely.
How do they help improve catalyst efficiency?
The balls create even gaps that let gas or liquid flow through without blocking. This helps the catalyst work better by spreading out the material evenly. They also stop the catalyst from moving or breaking apart.
Are they safe for high-temperature processes?
Yes. These balls can handle temperatures up to 1,700°C without cracking or deforming. They stay chemically neutral, so they won’t react with other materials in the system. This makes them reliable for long-term use in hot environments.
REQUEST A QUOTE
RELATED PRODUCTS
Custom High Purity Pink Alumina (Al2O3) Ceramic Wafer / Substrate
92% Alumina Ceramic Hexagonal Mosaic Lining Tile
Wear Resistant Alumina Ceramic Shaft for High-Speed Pumps
Alumina Ceramic Insulating Beads for Thermocouples
Custom Size Corrosion Resistant Alumina Ceramic Shaft