Next-Generation Ceramics: Unlocking Superior Properties for Industry

PRODUCT PARAMETERS
Description
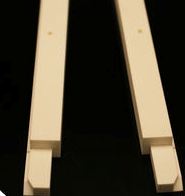
Overview of High Precision Alumina Ceramic Refractory Tube / Shaft for Boiler Pumps
Alumina Ceramic, or Aluminum Oxide (Al₂O₃), is the most widely used and versatile advanced ceramic material. Known for its excellent balance of mechanical, thermal, and electrical properties, it is a cost-effective solution for a vast array of demanding industrial applications. Alumina components are produced in purity levels ranging from 85% to 99.9%, with properties enhancing as purity increases.
Features of High Precision Alumina Ceramic Refractory Tube / Shaft for Boiler Pumps
- High Hardness & Wear Resistance: Offers exceptional resistance to abrasion and mechanical wear.
- Excellent Electrical Insulation: Maintains high electrical resistivity even at elevated temperatures.
- Good Thermal Conductivity: (For a ceramic) effectively dissipates heat, especially in higher purity grades.
- High Compressive Strength: Capable of withstanding significant mechanical loads.
- Chemical Inertness: Highly resistant to corrosion from acids, alkalis, and molten metals.
- Cost-Effectiveness: Provides superior performance at a lower cost compared to many other technical ceramics.
Specifications of High Precision Alumina Ceramic Refractory Tube / Shaft for Boiler Pumps
These high accuracy alumina ceramic refractory tubes and shafts are constructed hard for demanding central heating boiler pump applications. They manage severe warmth and severe conditions dependably. Alumina ceramic is the key material here. It provides impressive efficiency characteristics. This material holds up against really high temperatures. It won’t thaw or weaken easily under extreme central heating boiler heat. Alumina ceramic also withstands chemical deterioration successfully. It does not respond severely with aggressive liquids or gases usual in central heating boiler systems. This prevents degradation in time.
Dimensional stability is one more major benefit. These tubes and shafts hold their sizes and shape specifically. They do not warp or reduce considerably under thermal stress. This accuracy is crucial for smooth pump procedure. Tight resistances are preserved continually. Parts fit flawlessly and work appropriately. Alumina ceramic is really hard too. It withstands wear and abrasion magnificently. This indicates a much longer life span. Components last much longer also in abrasive atmospheres. They require changing less often.
Thermal shock resistance is excellent. These components deal with quick temperature level modifications without breaking. Central heating boilers can experience quick heat spikes and drops. The alumina ceramic product deals well. Electrical insulation homes are intrinsic. Alumina ceramic is naturally non-conductive. This avoids electric concerns within the pump assembly. Surface finishes are typically very smooth. This decreases rubbing and wear on moving components. Personalized sizes and shapes are commonly readily available. Details application requirements can be satisfied.
These tubes and shafts are manufactured utilizing sophisticated sintering procedures. This ensures high density and purity. The result is a durable, high-performance component. It fulfills the rigorous demands of boiler feed pumps. Dependability and durability are guaranteed. Upkeep expenses are lowered significantly. Operators gain assurance. Central heating boiler systems run extra efficiently overall.
Applications of High Precision Alumina Ceramic Refractory Tube / Shaft for Boiler Pumps
High accuracy alumina ceramic refractory tubes and shafts are important parts for boiler pumps. These parts encounter very harsh problems. Boiler settings involve heats and harsh products. Criterion steel components typically fall short here. They break too quick. They can wear away. They might deform under heat anxiety. Alumina ceramic resolves these problems properly. It manages severe warmth incredibly well. It withstands thermal shock. Sudden temperature level adjustments do not split it conveniently. This material is also extremely difficult. It holds up against abrasive wear better than metals. Abrasive slurries damage pump parts. Ceramic components last a lot longer. Chemical resistance is an additional huge benefit. Alumina ceramic does not react with most chemicals found in central heating boiler systems. It stays stable. It does not break down. This makes sure trusted procedure with time. Precision manufacturing is essential. These tubes and shafts are made to precise dimensions. They fit pump settings up flawlessly. Limited resistances are preserved. This protects against leaks. It lowers vibration. It enhances general pump efficiency. Seals work better with smooth, exact ceramic surfaces. Friction is reduced. Power loss decreases. Maintenance expenses drop. Pump downtime is decreased. Operators conserve money. Utilizing these ceramic parts suggests longer service life for the pump. Dependability improves dramatically. Boiler operations end up being smoother. These alumina ceramic components are a smart upgrade. They deal with the most difficult central heating boiler pump tasks.

Company Profile
Synthetic-chemical focus on the research and development, production and sales of ceramic products, serving the electronics, ceramics, chemical and other industries. Since its establishment in 2015, the company has been committed to providing customers with the best products and services, and has become a leader in the industry through continuous technological innovation and strict quality management.
Our products includes but not limited to Aluminum Nitride, Aluminum Oxide, Boron Carbide, Boron Nitride, Ceramic Crucible, ect. If you are interested in any type of these, please feel free to contact us.

Payment Methods
T/T, Western Union, Paypal, Credit Card etc.
Shipment Methods
By air, by sea, by express, as customers request.
5 FAQs of High Precision Alumina Ceramic Refractory Tube / Shaft for Boiler Pumps
What is this alumina ceramic tube used for?
This alumina ceramic tube handles boiler pump shafts. Boiler pumps face tough conditions. High heat and chemical attack are common. Metal parts often fail here. This ceramic tube solves that problem. It withstands extreme environments much better.
Why use alumina ceramic instead of metal?
Alumina ceramic handles extreme heat. It resists temperatures over 1500°C easily. Metal parts soften or melt at these temperatures. Alumina also fights off chemical attack. Boiler water contains harsh chemicals. These chemicals quickly corrode metal. Alumina ceramic ignores them. This means the tube lasts much longer.
How precise are these ceramic tubes?
These tubes are made to high precision. They have very tight size tolerances. Their surfaces are very smooth. This precision is crucial for boiler pumps. Pump shafts must spin freely and seal well. A poorly fitting shaft causes leaks or jams. Our precise tubes ensure smooth, reliable operation.
Is this ceramic material strong enough?
Yes, alumina ceramic is very strong. It has high mechanical strength. It also resists wear extremely well. Boiler pump shafts face constant friction. Metal shafts wear down over time. Alumina ceramic withstands this wear much longer. This reduces downtime and maintenance costs.
Does the ceramic tube conduct electricity?
No, alumina ceramic is an electrical insulator. It does not conduct electricity. This is an important safety feature. Boiler systems use electrical components. Preventing electrical conduction avoids short circuits. This makes the pump system safer overall.
REQUEST A QUOTE
RELATED PRODUCTS
Zirconia-Gravel Alumina Ceramic Basket Gemstone – 38.1x25x23mm
96% Alumina (Al2O3) High Purity Ceramic Substrate Plate
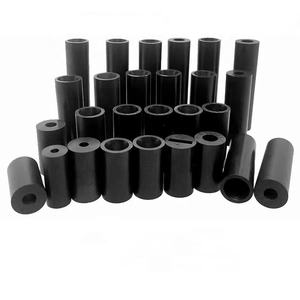
Factory Customized High Purity 99.5% Al2O3 Ceramic Ring
Abrasive Grade Aluminum Oxide Particle Materials
Alumina Ceramic Tube for Industry