Next-Generation Ceramics: Unlocking Superior Properties for Industry

PRODUCT PARAMETERS
Description
Overview of Essential 4N High-Purity Alumina for Environmental Technologies
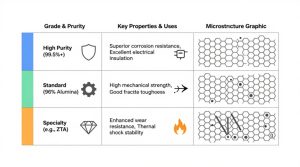
Alumina Ceramic, or Aluminum Oxide (Al₂O₃), is the most widely used and versatile advanced ceramic material. Known for its excellent balance of mechanical, thermal, and electrical properties, it is a cost-effective solution for a vast array of demanding industrial applications. Alumina components are produced in purity levels ranging from 85% to 99.9%, with properties enhancing as purity increases.
Features of Essential 4N High-Purity Alumina for Environmental Technologies
- High Hardness & Wear Resistance: Offers exceptional resistance to abrasion and mechanical wear.
- Excellent Electrical Insulation: Maintains high electrical resistivity even at elevated temperatures.
- Good Thermal Conductivity: (For a ceramic) effectively dissipates heat, especially in higher purity grades.
- High Compressive Strength: Capable of withstanding significant mechanical loads.
- Chemical Inertness: Highly resistant to corrosion from acids, alkalis, and molten metals.
- Cost-Effectiveness: Provides superior performance at a lower cost compared to many other technical ceramics.
Specifications of Essential 4N High-Purity Alumina for Environmental Technologies
Requirements of Crucial 4N High-Purity Alumina for Environmental Technologies
Pureness and Composition
Crucial 4N High-Purity Alumina includes at the very least 99.99% light weight aluminum oxide (Al ₂ O TWO). This degree of purity meets the “4N” requirement, indicating just 100 parts per million (ppm) or much less of complete contaminations exist. Secret micronutrient such as salt, iron, silicon, and calcium are each kept listed below 5 ppm. Such rigorous control makes sure consistent performance in demanding ecological applications.
Physical Characteristics
The product appears as a great white powder with a normal fragment size varying from 0.5 to 2.0 micrometers. Its details surface area drops between 3 and 8 m ²/ g, which supports high reactivity and reliable interaction with toxins. The alumina has low moisture content– normally under 0.1%– and preserves superb flowability for easy handling throughout making processes.
Efficiency in Environmental Applications
This high-purity alumina is excellent for use in advanced filtration systems, catalytic converters, and adsorbent media. Its clean chemical account stops unwanted side responses. The uniform bit framework improves surface contact with contaminants like hefty metals or acidic gases. Since it does not have reactive pollutants, it assists prolong the life of environmental tools and enhances general system dependability.
Quality control
Every batch goes through strenuous testing using ICP-MS and XRF methods to validate pureness and composition. Production complies with ISO 9001 criteria, guaranteeing full traceability from raw material to end product. Product packaging is done in secured, moisture-resistant containers to preserve top quality throughout storage and transportation.
Vital 4N High-Purity Alumina provides trustworthy efficiency where even minor impurities can jeopardize results. It is engineered particularly for engineers and scientists that need accuracy, security, and compliance in ecological innovation services.
Applications of Essential 4N High-Purity Alumina for Environmental Technologies
Applications of Important 4N High-Purity Alumina for Environmental Technologies
Clean Water Therapy
Important 4N high-purity alumina plays a vital role in water purification systems. Its ultra-clean surface removes heavy steels, fluoride, and various other harmful contaminants from alcohol consumption water. Metropolitan therapy plants and household filters use this product due to the fact that it functions dependably and lasts a long time.
Air Contamination Control
This alumina likewise helps tidy industrial exhaust gases. Factories use it as an assistance material in catalytic converters that break down nitrogen oxides and volatile natural compounds. Due to the fact that it has extremely couple of pollutants, it does not conflict with chain reactions. This makes exhaust control systems a lot more reliable and stable over time.
Advanced Purification Media
In membrane layer and ceramic filters, 4N high-purity alumina supplies a solid, chemically inert foundation. It resists corrosion from acids and bases, which is essential in rough wastewater environments. Its consistent pore framework makes certain consistent flow and reliable bit capture without blocking.
Support for Environment-friendly Catalysts
Numerous eco-friendly chemical processes rely upon catalysts improved high-purity alumina. The product’s thermal security permits it to deal with heats throughout regrowth cycles. Scientist choose it for establishing new stimulants that transform waste into beneficial power or reduce greenhouse gas discharges.
Sensing Unit and Monitoring Devices
Environmental sensors often consist of 4N alumina elements. Its electric insulation and mechanical strength make it ideal for real estate sensitive discovery components. These devices check air and water quality in genuine time, assisting cities and industries stay within safety and security limits.

Company Profile
Synthetic-chemical focus on the research and development, production and sales of ceramic products, serving the electronics, ceramics, chemical and other industries. Since its establishment in 2015, the company has been committed to providing customers with the best products and services, and has become a leader in the industry through continuous technological innovation and strict quality management.
Our products includes but not limited to Aluminum Nitride, Aluminum Oxide, Boron Carbide, Boron Nitride, Ceramic Crucible, ect. If you are interested in any type of these, please feel free to contact us.

Payment Methods
T/T, Western Union, Paypal, Credit Card etc.
Shipment Methods
By air, by sea, by express, as customers request.
5 FAQs of Essential 4N High-Purity Alumina for Environmental Technologies
Frequently Asked Questions: Essential 4N High-Purity Alumina for Environmental Technologies
What is Essential 4N High-Purity Alumina?
Essential 4N High-Purity Alumina contains 99.99% pure aluminum oxide. It has very low levels of impurities like sodium, iron, and silicon. This makes it ideal for use in sensitive environmental applications where material purity matters.
Why is high purity important in environmental tech?
Impurities can interfere with chemical reactions or reduce the performance of filtration and catalytic systems. Using 4N alumina ensures consistent results. It helps systems work longer and more efficiently without unwanted side effects.
Where is this alumina used?
It is used in water purification membranes, catalyst supports, and advanced ceramic filters. These applications rely on stable, inert materials that do not leach contaminants. Essential 4N alumina meets those needs reliably.
How does it compare to standard-grade alumina?
Standard-grade alumina often contains more impurities. Those can degrade performance over time. Essential 4N alumina offers better thermal stability, chemical resistance, and mechanical strength. This leads to longer service life and lower maintenance costs.
Is Essential 4N alumina safe for the environment?
Yes. The material itself is non-toxic and chemically stable. Because it does not release harmful substances during use, it supports clean and sustainable environmental technologies. Its production also follows strict quality controls to minimize ecological impact.
REQUEST A QUOTE
RELATED PRODUCTS
Wear Resistant Alumina Ceramic Shaft for High-Speed Pumps
Alumina Ceramic Insulation Substrate Plate
Low Sodium White Fused Corundum for Refractory
Professional Spherical Alumina Powder for Thermal Interface Materials
High Hardness, Chemically Stable Alumina Ceramic Round Shaft