Next-Generation Ceramics: Unlocking Superior Properties for Industry

PRODUCT PARAMETERS
Description
Overview of Raw Materials of Regular Alumina (High Al2O3) for Optical Components
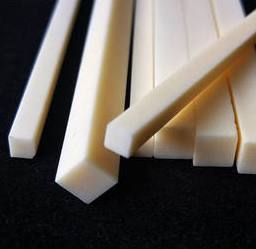
Alumina Ceramic, or Aluminum Oxide (Al₂O₃), is the most widely used and versatile advanced ceramic material. Known for its excellent balance of mechanical, thermal, and electrical properties, it is a cost-effective solution for a vast array of demanding industrial applications. Alumina components are produced in purity levels ranging from 85% to 99.9%, with properties enhancing as purity increases.
Features of Raw Materials of Regular Alumina (High Al2O3) for Optical Components
- High Hardness & Wear Resistance: Offers exceptional resistance to abrasion and mechanical wear.
- Excellent Electrical Insulation: Maintains high electrical resistivity even at elevated temperatures.
- Good Thermal Conductivity: (For a ceramic) effectively dissipates heat, especially in higher purity grades.
- High Compressive Strength: Capable of withstanding significant mechanical loads.
- Chemical Inertness: Highly resistant to corrosion from acids, alkalis, and molten metals.
- Cost-Effectiveness: Provides superior performance at a lower cost compared to many other technical ceramics.
Specifications of Raw Materials of Regular Alumina (High Al2O3) for Optical Components
Specs of Raw Products: Regular Alumina (High Al Two O TWO) for Optical Parts
Chemical Pureness
Al two O five content need to go to the very least 99.8%.
Other elements are purely limited. Salt (Na) need to not surpass 50 ppm. Iron (Fe) need to remain listed below 20 ppm. Silicon (Si) and calcium (Ca) each must continue to be under 30 ppm. These limitations make sure minimal light absorption and scattering in completed optical parts.
Physical Characteristics
The raw material appears as a fine white powder. Particle size is snugly regulated. Ordinary bit diameter ranges from 0.3 to 0.6 micrometers. The circulation is narrow to support consistent sintering. Faucet density falls in between 0.8 and 1.1 g/cm FOUR. High packaging density helps in reducing porosity during creating.
Crystalline Framework
Product must be totally alpha-phase alumina. No gamma or other transitional phases are permitted. Alpha-phase makes sure thermal security and mechanical stamina after sintering. X-ray diffraction verifies stage purity prior to approval.
Moisture and Volatiles
Wetness material should be less than 0.1% by weight. Excess water can cause flaws during high-temperature processing. All batches undertake drying out and evaluating under standard lab conditions.
Contamination Control
Resources are taken care of in cleanroom environments. Product packaging utilizes sealed, non-reactive containers. Each set lugs a complete traceability document. Distributors need to license compliance with optical-grade requirements. Incoming great deals are examined for metal and natural deposits.
Handling Suitability
This alumina quality is created for pressing, casting, or injection molding. It flows well and compacts equally. After sintering at 1600– 1700 ° C, parts show high openness and low haze. Surface area surface satisfies demands for lenses, home windows, and laser elements.
Applications of Raw Materials of Regular Alumina (High Al2O3) for Optical Components
Applications of Raw Products of Regular Alumina (High Al Two O FOUR) for Optical Elements
Why High-Purity Alumina Issues
Routine alumina with high Al two O four content is a vital resources in making optical elements. Its strong framework and steady chemistry make it ideal for components that should remain clear and exact under hard conditions. This product stands up to warm, wear, and rust– vital traits for lenses, windows, and sensors made use of sought after environments.
Use in Transparent Ceramics
One major use remains in transparent ceramics. When processed properly, high-purity alumina ends up being optically clear. It sends light well throughout noticeable and near-infrared ranges. These ceramics replace glass in applications needing much better stamina or higher temperature resistance. Instances consist of safety windows for army systems, aerospace sensors, and industrial evaluation devices.
Function in Substratums and Insulators
Alumina additionally works as a base for optical tools. Its smooth surface and electrical insulation support thin-film finishings made use of in filters, mirrors, and laser elements. Due to the fact that it does not warp quickly with warmth, it keeps optical alignment steady with time. This stability issues in accuracy tools like spectrometers and medical imaging systems.
Assistance for Specialized Coatings
Producers use specialty layers onto alumina substrates to improve efficiency. Anti-reflective, scratch-resistant, or conductive layers bond well to its surface. The result is a resilient part that satisfies rigorous optical requirements while handling mechanical stress or rough chemicals.
Integrity Throughout Industries
From protection to health care, sectors depend on high-Al two O two alumina for reputable optical performance. Its equilibrium of clearness, durability, and thermal security fills up spaces where typical products fall short. As optical systems grow more complex, this basic material continues to play a silent however important duty behind the scenes.

Company Profile
Synthetic-chemical focus on the research and development, production and sales of ceramic products, serving the electronics, ceramics, chemical and other industries. Since its establishment in 2015, the company has been committed to providing customers with the best products and services, and has become a leader in the industry through continuous technological innovation and strict quality management.
Our products includes but not limited to Aluminum Nitride, Aluminum Oxide, Boron Carbide, Boron Nitride, Ceramic Crucible, ect. If you are interested in any type of these, please feel free to contact us.

Payment Methods
T/T, Western Union, Paypal, Credit Card etc.
Shipment Methods
By air, by sea, by express, as customers request.
5 FAQs of Raw Materials of Regular Alumina (High Al2O3) for Optical Components
Frequently Asked Questions: Raw Materials of Regular Alumina (High Al₂O₃) for Optical Components
What is regular alumina with high Al₂O₃ content?
Regular alumina with high Al₂O₃ means the material contains at least 99.5% aluminum oxide. This high purity level gives it excellent optical clarity and thermal stability. It is widely used in lenses, windows, and other optical parts.
Why is high purity important for optical applications?
Impurities scatter or absorb light. Even small amounts can reduce transmission and distort images. High-purity alumina minimizes these effects. That’s why it delivers clear, consistent performance in demanding optical systems.
How is this alumina processed for optical use?
The raw powder is carefully milled and formed into shapes like blanks or rods. It then goes through high-temperature sintering. After sintering, the part is polished to optical-grade smoothness. Every step controls contamination and density to maintain quality.
Can regular high-Al₂O₃ alumina replace single-crystal sapphire?
It depends on the application. Polycrystalline alumina offers good optical properties at lower cost than sapphire. But sapphire has higher strength and better transmission in UV ranges. For many visible-light uses, high-purity alumina works well and saves money.
What standards apply to raw materials for optical alumina?
Reputable suppliers follow strict chemical and physical specs. Key checks include Al₂O₃ percentage, grain size, and trace elements like sodium or silica. Certifications such as ISO 9001 help ensure batch-to-batch consistency. Always ask for material test reports before buying.
REQUEST A QUOTE
RELATED PRODUCTS
Custom Industrial Alumina Ceramic Spacer
High Brazing Strength Metalized Alumina Ceramic Parts
High Hardness, Chemically Stable Alumina Ceramic Round Shaft
Large Size CNC Machined Alumina (Aluminum Oxide) Industrial Plate / Sheet
Alumina Ceramic Shaft & Bushing for Oxygen Sensors