Next-Generation Ceramics: Unlocking Superior Properties for Industry

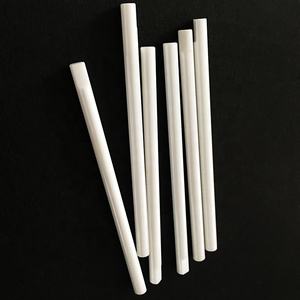
PRODUCT PARAMETERS
Description
Overview of High Hardness, Chemically Stable Alumina Ceramic Shaft for Boiler Pumps
Alumina Ceramic, or Aluminum Oxide (Al₂O₃), is the most widely used and versatile advanced ceramic material. Known for its excellent balance of mechanical, thermal, and electrical properties, it is a cost-effective solution for a vast array of demanding industrial applications. Alumina components are produced in purity levels ranging from 85% to 99.9%, with properties enhancing as purity increases.
Features of High Hardness, Chemically Stable Alumina Ceramic Shaft for Boiler Pumps
- High Hardness & Wear Resistance: Offers exceptional resistance to abrasion and mechanical wear.
- Excellent Electrical Insulation: Maintains high electrical resistivity even at elevated temperatures.
- Good Thermal Conductivity: (For a ceramic) effectively dissipates heat, especially in higher purity grades.
- High Compressive Strength: Capable of withstanding significant mechanical loads.
- Chemical Inertness: Highly resistant to corrosion from acids, alkalis, and molten metals.
- Cost-Effectiveness: Provides superior performance at a lower cost compared to many other technical ceramics.
Specifications of High Hardness, Chemically Stable Alumina Ceramic Shaft for Boiler Pumps
High Firmness, Chemically Secure Alumina Ceramic Shaft for Central Heating Boiler Pumps
Product and Firmness
This shaft is made from high-purity alumina ceramic. It has a firmness of 1500– 1700 HV, which is much more than the majority of steels. The extreme hardness helps the shaft resist wear even under hefty use. It keeps its shape and surface area smooth over extended periods.
Chemical Security
Alumina ceramic does not respond with water, steam, or usual boiler chemicals. It stays secure in high-temperature and high-pressure atmospheres. This makes it suitable for central heating boiler pump systems where rust can damage steel components promptly. The shaft will certainly not corrosion or weaken when exposed to rough liquids.
Thermal Efficiency
The shaft handles temperature levels approximately 1600 ° C without losing strength. It additionally has low thermal expansion. That indicates it won’t warp or fracture when the temperature level modifications fast. This stability ensures dependable operation sought after central heating boiler problems.
Precision and Surface Area Finish
Each shaft is ground to tight tolerances. The surface area roughness is maintained below Ra 0.2 µm. This smooth coating decreases rubbing and prevents leaks in the pump seal area. It additionally helps expand the life of neighboring components like seals and bearings.
Trick Specifications
Product: ≥ 99.5% Al ₂ O SIX.
Density: 3.95 g/cm FIVE.
Flexural Toughness: 350– 400 MPa.
Compressive Stamina: ≥ 2000 MPa.
Max Operating Temperature: 1600 ° C.
Thermal Conductivity: 28– 30 W/m · K. Electrical Resistivity: > 10 ¹⁴ Ω · cm.
This ceramic shaft provides central heating boiler pumps better reliability, longer life span, and reduced maintenance expenses contrasted to typical steel shafts.
Applications of High Hardness, Chemically Stable Alumina Ceramic Shaft for Boiler Pumps
High Hardness, Chemically Steady Alumina Porcelain Shaft for Central Heating Boiler Pumps
Engineered for Extreme Conditions
Central heating boiler pumps run under high pressure and temperature. They also encounter harsh water and steam. Criterion steel shafts break quickly in these problems. That is why many engineers currently pick alumina ceramic shafts.
Alumina ceramic has extremely high solidity. It withstands wear far better than the majority of steels. This indicates the shaft lasts much longer. Upkeep costs decrease. Downtime goes down also.
Secure Against Chemical Strike
Water in boilers frequently includes liquified salts and oxygen. These can corrode steel parts gradually. Alumina ceramic does not react with these chemicals. It stays solid and intact even after years of use. There is no rust. There is no pitting.
This chemical security makes alumina perfect for feedwater pumps, blood circulation pumps, and condensate return systems. The shaft maintains its form and smooth surface area. Pump effectiveness remains high.
Accuracy Performance
These ceramic shafts are made to tight resistances. Their surface area coating is smooth. This minimizes friction inside the pump. Much less power is wasted as warm. The motor runs cooler and makes use of much less power.
Since alumina is stiff and steady, it does not flex or warp easily. Vibration remains reduced. Noise degrees drop. The whole pump runs much more silently and reliably.
Constructed to Last
Alumina ceramic shafts deal with thermal shock well. They work smoothly from chilly beginning to full operating temperature level. No splitting. No unexpected failing.
They likewise resist scaling and fouling. Down payments do not stick easily to the surface area. Cleansing is simpler. Circulation stays regular.
Facilities that utilize these shafts report fewer break downs and longer solution periods. Operators spend less time on repair work. Manufacturing maintains relocating without interruption.

Company Profile
Synthetic-chemical focus on the research and development, production and sales of ceramic products, serving the electronics, ceramics, chemical and other industries. Since its establishment in 2015, the company has been committed to providing customers with the best products and services, and has become a leader in the industry through continuous technological innovation and strict quality management.
Our products includes but not limited to Aluminum Nitride, Aluminum Oxide, Boron Carbide, Boron Nitride, Ceramic Crucible, ect. If you are interested in any type of these, please feel free to contact us.

Payment Methods
T/T, Western Union, Paypal, Credit Card etc.
Shipment Methods
By air, by sea, by express, as customers request.
5 FAQs of High Hardness, Chemically Stable Alumina Ceramic Shaft for Boiler Pumps
Frequently Asked Questions: High Hardness, Chemically Stable Alumina Ceramic Shaft for Boiler Pumps
Why choose an alumina ceramic shaft over metal?
Metal shafts wear out fast in hot, corrosive boiler water. Alumina ceramic resists corrosion and stays strong at high temperatures. It lasts much longer and needs less maintenance.
How hard is the alumina ceramic shaft?
This shaft uses 95–99% pure alumina. Its hardness is close to sapphire—much harder than steel. That means it resists scratches, abrasion, and surface damage even under tough conditions.
Will it handle high-pressure boiler environments?
Yes. The shaft is made through precision sintering. This gives it high compressive strength and dimensional stability. It works reliably in high-pressure, high-temperature boiler systems without warping or cracking.
Is it safe for use with water treatment chemicals?
Absolutely. Alumina ceramic is chemically inert. It does not react with common boiler water additives like oxygen scavengers or pH adjusters. No leaching. No degradation. Just stable performance over time.
What about installation and compatibility?
The shaft is designed to match standard pump dimensions. You can replace your old metal shaft directly without changing the whole pump. We offer tight tolerance control so it fits smoothly and runs quietly from day one.
REQUEST A QUOTE
RELATED PRODUCTS
Raw Material for Refractories: Calcined Bauxite Alumina Grains (Al2O3)
Zirconia-Gravel Coated Alumina Ceramic Basket Gemstone
4N High Purity Aluminum Oxide (Al2O3 ≥99.99%) for Electronic Ceramics
Zirconia Ceramic Basket Gemstone with Alumina Coating
Whole Best White Alumina (Al2O3) Polishing Powder from China