Next-Generation Ceramics: Unlocking Superior Properties for Industry

PRODUCT PARAMETERS
Description
Overview of High-Purity Alumina for Optical Coatings
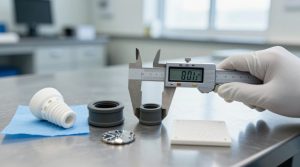
Alumina Ceramic, or Aluminum Oxide (Al₂O₃), is the most widely used and versatile advanced ceramic material. Known for its excellent balance of mechanical, thermal, and electrical properties, it is a cost-effective solution for a vast array of demanding industrial applications. Alumina components are produced in purity levels ranging from 85% to 99.9%, with properties enhancing as purity increases.
Features of High-Purity Alumina for Optical Coatings
- High Hardness & Wear Resistance: Offers exceptional resistance to abrasion and mechanical wear.
- Excellent Electrical Insulation: Maintains high electrical resistivity even at elevated temperatures.
- Good Thermal Conductivity: (For a ceramic) effectively dissipates heat, especially in higher purity grades.
- High Compressive Strength: Capable of withstanding significant mechanical loads.
- Chemical Inertness: Highly resistant to corrosion from acids, alkalis, and molten metals.
- Cost-Effectiveness: Provides superior performance at a lower cost compared to many other technical ceramics.
Specifications of High-Purity Alumina for Optical Coatings
High-Purity Alumina for Optical Coatings
Purity and Structure
This high-purity alumina has a minimum of 99.99% light weight aluminum oxide (Al two O FOUR). Trace impurities like sodium, iron, and silicon are maintained listed below 10 parts per million (ppm). Such strict control makes certain marginal light absorption and spreading in optical applications.
Fragment Size and Morphology
The product includes a narrow fragment size circulation, commonly in between 0.2 and 0.5 micrometers. Particles are round and non-agglomerated. This uniform form aids develop smooth, thick thin movies during deposition procedures like electron-beam dissipation or sputtering.
Crystal Structure
The alumina is amorphous as provided, which supports consistent movie formation without unwanted crystalline phases. Users can harden the material if a details crystalline framework– such as gamma or alpha phase– is required after finishing.
Moisture and Volatiles
Wetness content stays under 0.05% by weight. Reduced degrees of volatiles stop outgassing throughout vacuum deposition, minimizing problems and pinholes in the final covering.
Product packaging and Handling
Each batch comes in sealed, moisture-resistant containers under inert gas. This shields the powder from moisture and contamination. Always handle in a tidy, dry atmosphere to maintain efficiency.
Applications
Strong efficiency makes this alumina suitable for anti-reflective coverings, safety layers on lenses, laser optics, and accuracy filters. Its stability across UV to infrared wavelengths sustains use in demanding clinical and industrial systems.
Quality Assurance
Every great deal goes through rigorous screening utilizing ICP-MS for trace elements, BET for area, and XRD for phase analysis. Certificates of Evaluation are offered with each shipment to confirm conformity with optical-grade requirements.
Applications of High-Purity Alumina for Optical Coatings
Applications of High-Purity Alumina for Optical Coatings
Why High-Purity Alumina Issues
High-purity alumina is a vital material in making optical layers. These finishings take place lenses, mirrors, and other optical parts. They help regulate how light steps through or shows off a surface area. Because high-purity alumina has really couple of contaminations, it offers clear, secure outcomes. This makes it suitable for sensitive optical systems.
Usage in Anti-Reflective Coatings
One significant use is in anti-reflective coverings. These coverings lowered glare and increase light transmission. Cams, spectacles, and solar panels all benefit from this. High-purity alumina aids produce thin, even layers that function well throughout different light wavelengths. The result is sharper images and better efficiency.
Role in Safety Layers
Optical parts commonly deal with harsh conditions like warmth, wetness, or scratches. High-purity alumina kinds hard, resilient films that shield delicate surfaces. It stays stable under high temperatures and does not degrade conveniently. This keeps optical tools functioning much longer without losing clarity.
Assistance for Accuracy Instruments
In clinical and clinical tools, even little flaws can cause big mistakes. High-purity alumina makes sure regular finish density and optical habits. Gadgets like microscopes, lasers, and fiber optics count on this precision. The product’s uniform structure aids keep precision in time.
Compatibility with Modern Production
This form of alumina functions well with typical covering methods like sputtering and evaporation. It bonds highly to glass and various other substrates. Manufacturers can produce big batches with tight quality assurance. That suggests reliable efficiency at scale, without added price or intricacy.
High-purity alumina stays a relied on option because it supplies both performance and dependability. Its clean make-up and physical security meet the strict demands these days’s optical modern technologies.

Company Profile
Synthetic-chemical focus on the research and development, production and sales of ceramic products, serving the electronics, ceramics, chemical and other industries. Since its establishment in 2015, the company has been committed to providing customers with the best products and services, and has become a leader in the industry through continuous technological innovation and strict quality management.
Our products includes but not limited to Aluminum Nitride, Aluminum Oxide, Boron Carbide, Boron Nitride, Ceramic Crucible, ect. If you are interested in any type of these, please feel free to contact us.

Payment Methods
T/T, Western Union, Paypal, Credit Card etc.
Shipment Methods
By air, by sea, by express, as customers request.
5 FAQs of High-Purity Alumina for Optical Coatings
What is high-purity alumina used for in optical coatings?
High-purity alumina is a key material in optical coatings. It helps control how light moves through lenses, mirrors, and other optical parts. Because it is very pure, it does not absorb much light. This makes coated surfaces clearer and more efficient.
Why does purity matter for optical-grade alumina?
Even tiny impurities can scatter or block light. That hurts performance. Optical-grade alumina must be 99.99% pure or higher. This level of purity keeps light transmission strong and prevents color shifts or haze in the final product.
How is high-purity alumina applied in coatings?
It is usually applied using physical vapor deposition (PVD) or sputtering. These methods turn solid alumina into a thin film on glass or other substrates. The result is a smooth, uniform layer that works well across different wavelengths of light.
Can high-purity alumina withstand harsh environments?
Yes. Alumina is hard, chemically stable, and resistant to heat and moisture. Coatings made from it last longer in tough conditions—like high humidity, extreme temperatures, or UV exposure—without degrading or peeling.
What industries rely on this material?
High-purity alumina is used in many fields. These include aerospace, defense, semiconductor manufacturing, laser systems, and precision optics. Any application needing reliable, high-performance coatings often chooses alumina for its balance of clarity, durability, and stability.
REQUEST A QUOTE
RELATED PRODUCTS
Alumina Ceramic Shaft & Bushing for Oxygen Sensors
Zirconia-Gravel Crafted Alumina Ceramic Basket Gemstone
Metalized Al2O3 Ceramic Substrate PCB for Antenna Components
Alumina Ceramic Lined Equipment for Mining & Mineral Processing
High Electrical Insulation 96% Alumina Ceramic Substrate