Next-Generation Ceramics: Unlocking Superior Properties for Industry

Defining the Unbreakable Workhorse
Aluminum oxide ceramic (Al2O3) is a synthetic, polycrystalline technical ceramic produced by consolidating alumina powder at extreme temperatures. It is not a clay-based pottery. It is an engineered material built for abuse. The industry defaults to aluminum oxide ceramic when a component must survive mechanical wear, high temperatures, and electrical stress simultaneously. Forget delicacy. This is industrial armor.
Core Properties: The Alumina Datasheet
People get this wrong. Alumina’s value isn’t in being the absolute best in any single category. Its power lies in a brutally effective balance of high performance across multiple critical axes.
Mechanical & Physical
- Hardness: ~9 on the Mohs scale. It will scratch steel, tungsten carbide, and most other materials it contacts. This directly translates to wear resistance.
- Strength: Compressive strength is exceptional (2000-4000 MPa). Its flexural/tensile strength is good, but not phenomenal. Design around its brittleness.
- Density: ~3.9 g/cm³. It’s heavier than many polymers and metals like aluminum, but lighter than steel.
Thermal & Electrical
- Melting Point: 2072°C (3762°F). It doesn’t melt. It retains its shape and strength in hellish thermal environments where metals fail.
- Thermal Conductivity: Moderate (~30 W/mK). It moves heat, but not like aluminum nitride ceramic or silicon carbide ceramic. This is a key differentiator.
- Electrical Insulation: Outstanding. High dielectric strength and volume resistivity even at elevated temperatures. It’s a bedrock material for electrical substrates and insulators.
The Alumina vs. The World: A Designer’s Reality Check
Choosing the wrong ceramic costs time and money. Here is the blunt, comparative truth.
| Material | Key Advantage vs. Alumina | Trade-Off / Reality Cheque |
|---|---|---|
| Zirconia (ZrO2) | Higher fracture toughness; less brittle. | Lower hardness, worse wear resistance. More expensive. Thermal conductivity is terrible. |
| Silicon Nitride (Si3N4) | Superior strength & toughness at high temp. | Significantly higher cost. Excellent for bearings and extreme engineering, but overkill for a simple wear plate. |
| Silicon Carbide (SiC) | Far superior thermal conductivity & oxidation resistance. | More difficult and expensive to machine. Can be more brittle in some grades (recrystallized silicon carbide ceramics). |
| Aluminum Nitride (AlN) | Exceptional thermal conductivity for an insulator. | Poor wear resistance. Expensive. Hydrolyzes in moist environments unless protected. |
| Boron Nitride (BN) | Excellent lubricity, thermal shock resistance. | Low mechanical strength. Often requires a special coating for boron nitride ceramic crucibles for longevity. |
How It’s Made: From Powder to Part
The performance is locked in during manufacturing. There are no shortcuts.
- Powder Preparation: High-purity Al2O3 powder is mixed with sintering aids and binders. Particle size distribution is critical.
- Forming: Pressing (uniaxial/isostatic) for simple shapes. Casting (slip, tape) for complex or thin shapes like substrates.
- Sintering: The green part is fired at 1600°C+. The powder particles fuse into a dense, polycrystalline structure. This step defines the final properties.
Grades Matter: Purity Dictates Performance
The percentage tells the story. A 99.5% alumina part is not just a ‘better’ version of a 96% part; it’s a different material with a different role.
| Grade / Purity | Typical Characteristics | Primary Applications |
|---|---|---|
| 85% – 94% Al2O3 | Lower cost, lower strength and hardness. Often contains silicate glass phase. | General wear parts, textile guides, low-stress insulators. |
| 96% Al2O3 | The industrial workhorse. Excellent balance of properties and cost. | Pump seals, wear plates, liners, thread guides, welding nozzles. |
| 99.5% – 99.8% Al2O3 | Higher strength, hardness, thermal conductivity. Superior corrosion resistance. | High-performance seals, critical medical devices, semiconductor wafer handling, advanced armor. |
| >99.9% Al2O3 | Highest purity, often translucent. Maximum electrical properties. | High-pressure sodium lamp envelopes, specialized labware, premium substrates. |
Where It Works: The Real-World Domains
Alumina isn’t a lab curiosity. It’s on the factory floor, inside your electronics, and in surgical suites.
Industrial Brutality
It replaces metal in applications where metal wears out. Pump seals and bearings in corrosive fluids. Blast nozzles for sandblasting. Liners for coal chutes and cyclones. As one machinist on Reddit put it, ‘We switched our wear plates to 96% alumina and stopped replacing them every quarter. It just sits there and takes the abuse.’ This is alumina’s home turf.
Electronics & Semiconductors
Its electrical insulation and decent thermal conductivity make it the default substrate for thick-film and thin-film circuits. It carries the current, handles the heat, and provides a stable, hermetic platform. Silicon carbide-bonded silicon nitride ceramics might handle more extreme heat, but alumina handles the everyday reality of circuit boards.
Medical & Biomedical
High-purity (99.5%+) alumina is biocompatible and bioinert. It’s the material for femoral heads in hip replacements and dental implants. It doesn’t react. It doesn’t corrode. It provides a hard, wear-resistant articulating surface. The feedback from the field is consistent: its long-term stability in the body is proven.
The Hard Truth: Limitations & Machining
You must respect its nature. Alumina is hard and brittle. You cannot machine it like metal.
- Grinding & Lapping: Diamond-impregnated tools are mandatory. This adds significant cost to complex shapes or tight tolerances.
- No Plastic Deformation: It will not bend or yield. It will fracture if overloaded. Designs must avoid tensile stress concentrations.
- Thermal Shock: While good, it’s not the best. Sudden, massive temperature differentials can crack it. Mullite ceramic or quartz ceramic often handle rapid cycling better.
The Final Verdict for Engineers
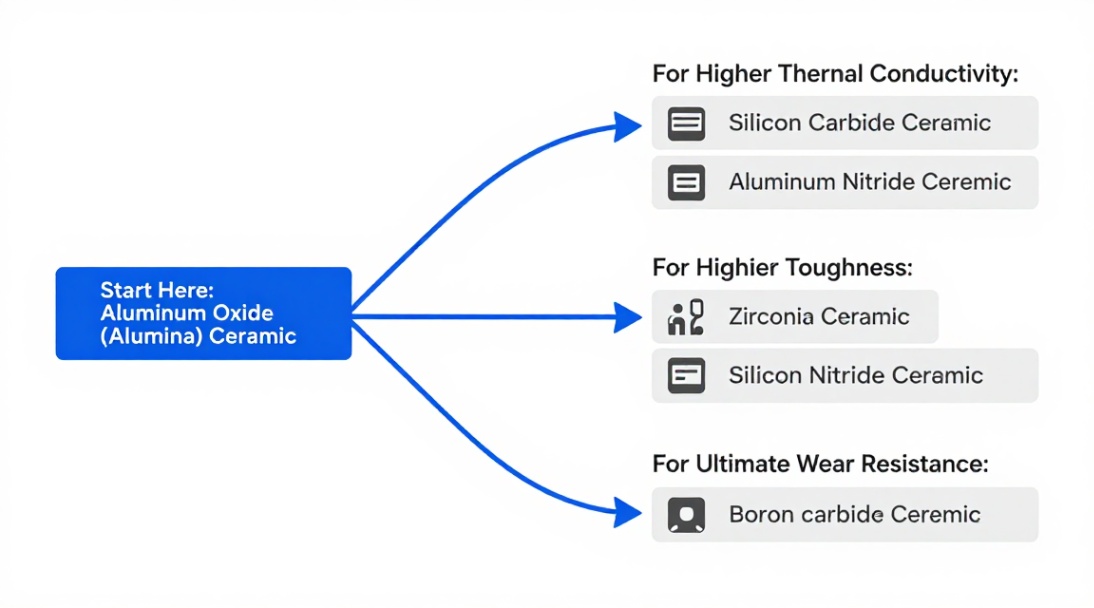
Aluminum oxide ceramic is the pragmatic, high-performance default. Start your material selection with alumina. Ask: Do I need higher thermal conductivity? Move to silicon carbide ceramic or aluminum nitride ceramic. Do I need higher toughness? Look at zirconia or silicon nitride ceramic. Need ultimate wear against abrasives? Boron carbide ceramic is harder.
But for the vast middle ground where cost, wear, temperature, and insulation intersect, alumina dominates. It’s not the sexiest ceramic. It is the most essential. Your job is to understand its rules and exploit its strengths.
Suppiler
Synthetic-chemical focus on the research and development, production and sales of ceramic products, serving the electronics, ceramics, chemical and other industries. Since its establishment in 2015, the company has been committed to providing customers with the best products and services, and has become a leader in the industry through continuous technological innovation and strict quality management.
Our products includes but not limited to Aluminum Nitride, Aluminum Oxide, Boron Carbide, Boron Nitride, Ceramic Crucible, ect. If you are interested in any type of these, please feel free to contact us.